Welding Consumables Supplier in India
Stainless, nickel alloy, duplex, carbon and alloy steel filler wire, electrodes, TIG rods and flux — AWS A5.4 / A5.9 / A5.14 / A5.1 with batch certificates.
What are welding consumables?
Welding consumables are the filler metals — covered electrodes, TIG and MIG wire, flux-cored wire and submerged-arc combinations — matched to the parent metal so the weld metal keeps the same strength and corrosion resistance. Selection follows the AWS classification: ER308L and E308L for 304, ER316L for 316, ER2209 for duplex 2205, ER2594 for super duplex and ERNiCrMo-3 for Inconel 625 and 6Mo grades.
Steelco Metal & Alloys supplies welding consumables from Mumbai across stainless, duplex, nickel alloy, titanium, carbon and chrome-moly steel, in sealed vacuum packs with batch test certificates and, where required, third-party approval documentation.
Consumable classifications we stock.
Filler metal is matched to the parent grade — the common pairings we supply are listed below.
Welding Consumables we hold in ready stock.
Stainless filler wire
ER308L, ER309L, ER316L, ER317L, ER347 and ER385 TIG and MIG wire to AWS A5.9.
Covered electrodes
E308L-16, E309L-16, E316L-16, E347-16 stainless electrodes to AWS A5.4.
Nickel alloy consumables
ERNiCrMo-3, ERNiCrMo-4, ERNiCu-7, ERNiCr-3 wire and matching electrodes to A5.14 / A5.11.
Duplex consumables
ER2209, ER2594 wire and E2209, E2594 electrodes for duplex and super duplex.
Carbon & alloy steel
E6013, E7018, E8018-B2, E9018-B3, E9015-B9 electrodes and ER70S-6 wire.
Flux & accessories
SAW flux, purge gas fittings, backing tape and tungsten electrodes.
Use our free metal weight calculator — bars, sheets, plates, pipes and sections.
Our welding consumable range
Ready stock across every mainstream form — dispatched with mill test certificates and full traceability from our Mumbai warehouse.
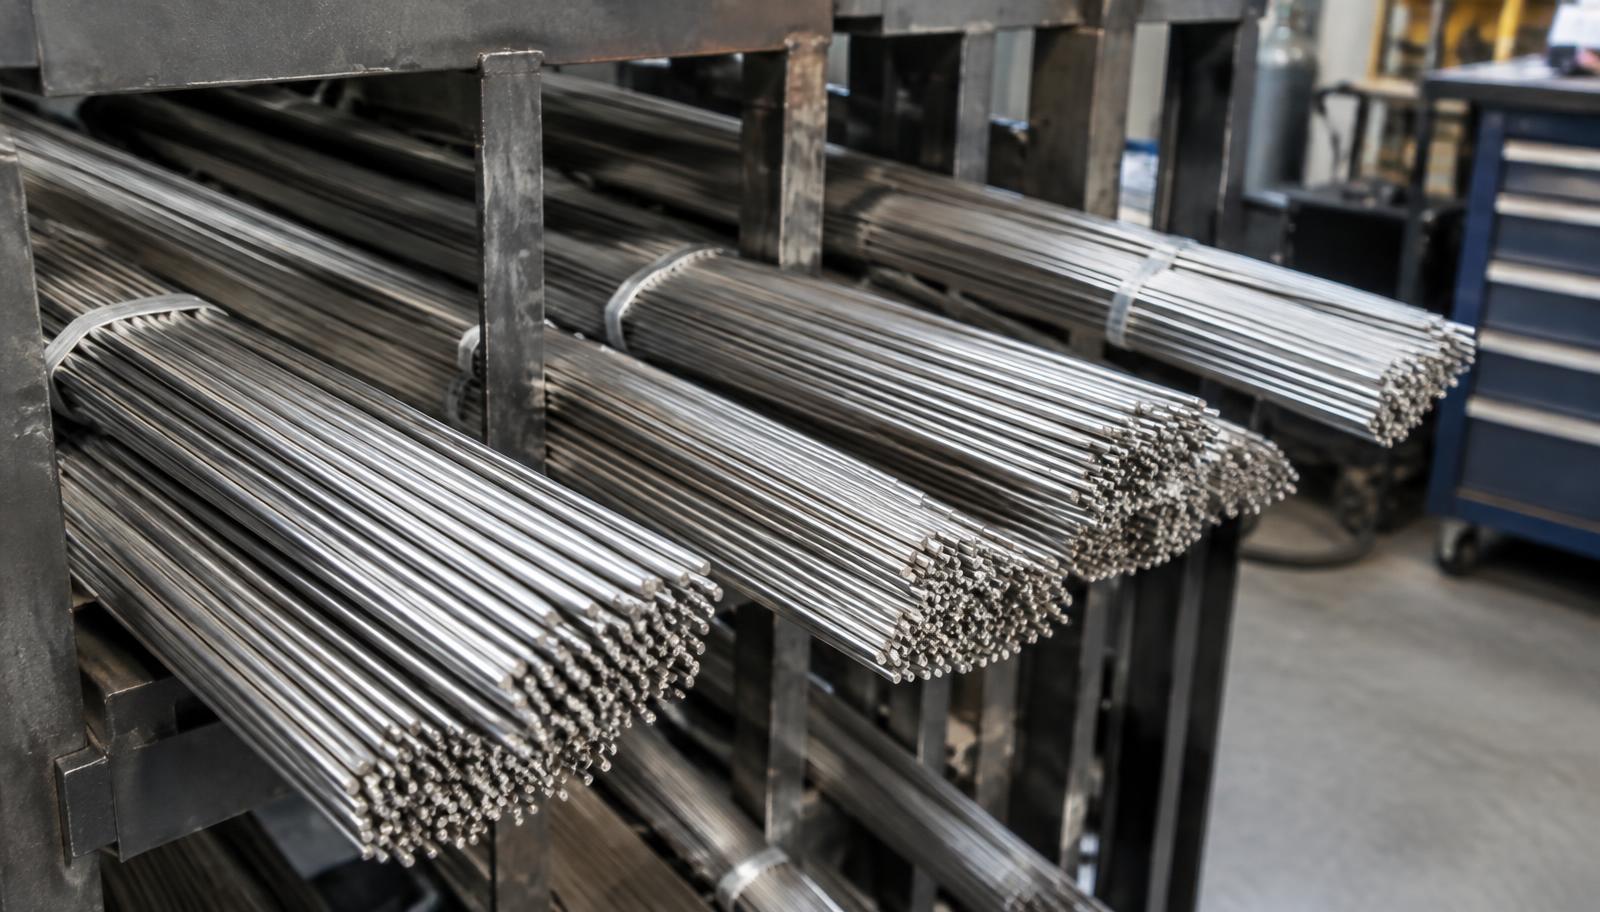
TIG Filler Rod
Ø 1.6 / 2.0 / 2.4 / 3.2 mm cut lengths.
Explore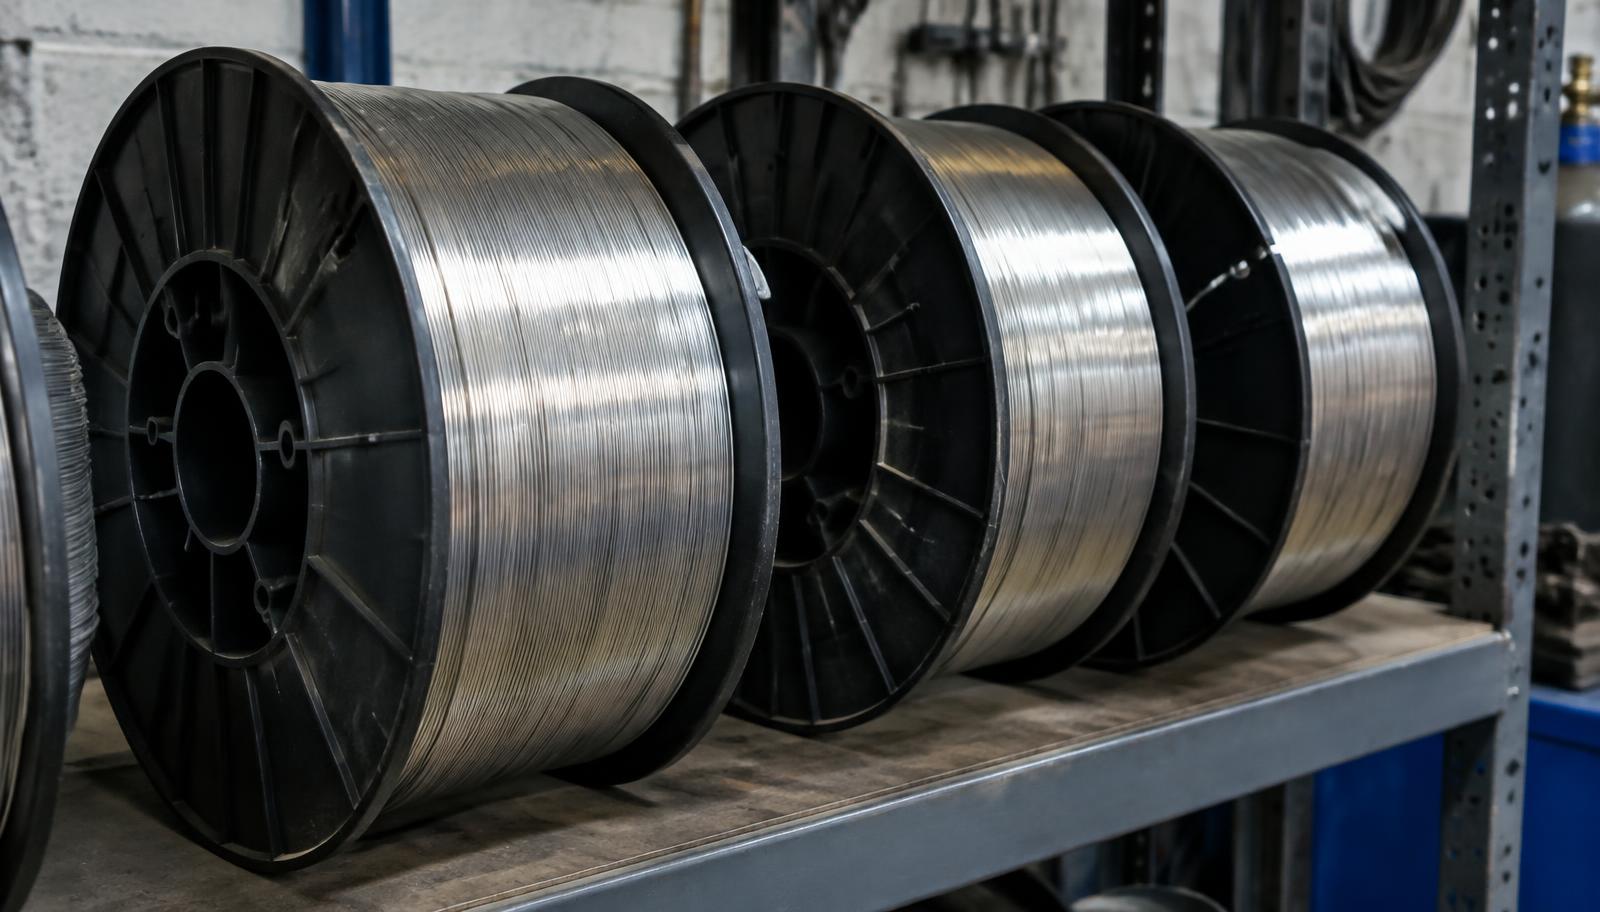
MIG Wire
Ø 0.8 / 1.0 / 1.2 mm on 12.5 kg spools.
Explore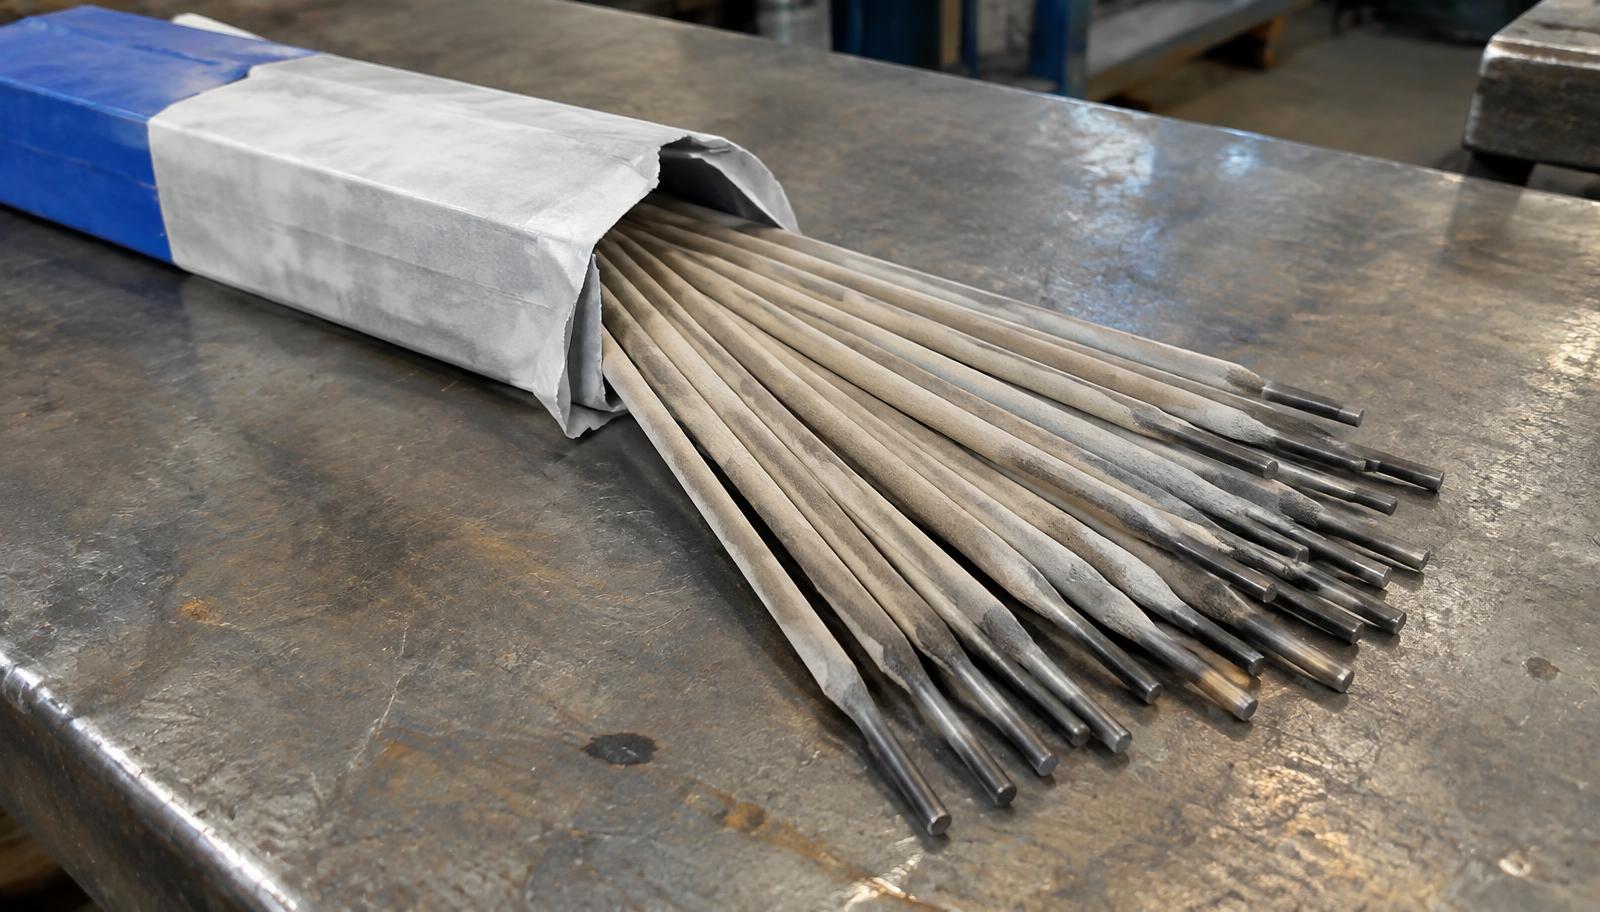
Covered Electrodes
Ø 2.5 / 3.15 / 4.0 mm in sealed packs.
Explore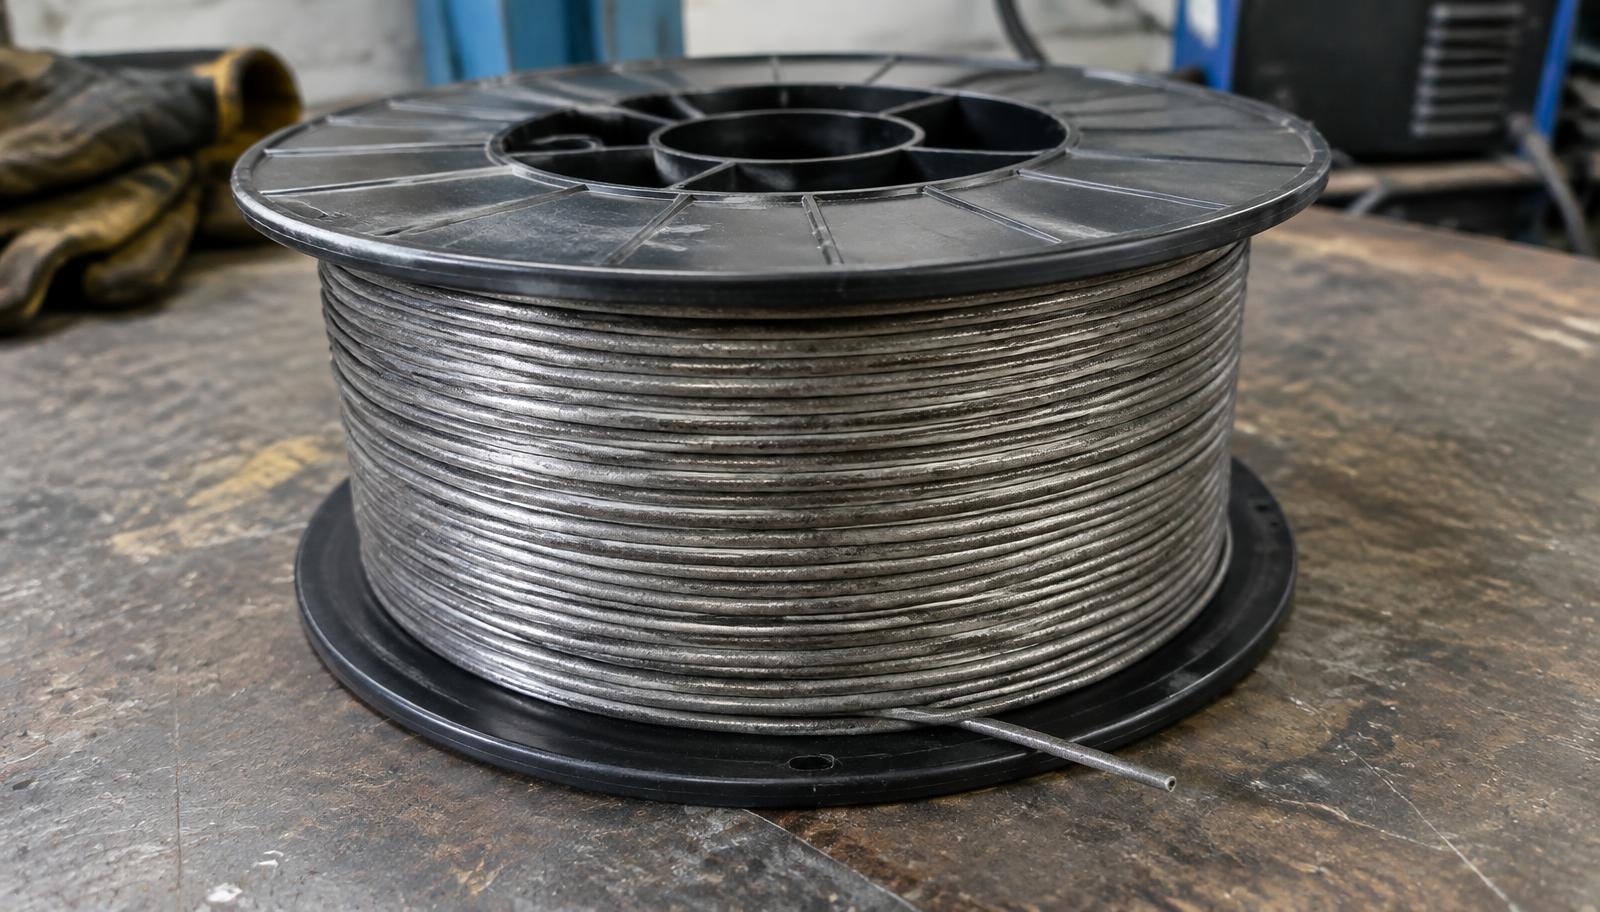
Flux-Cored Wire
Stainless and carbon steel FCAW wire.
Explore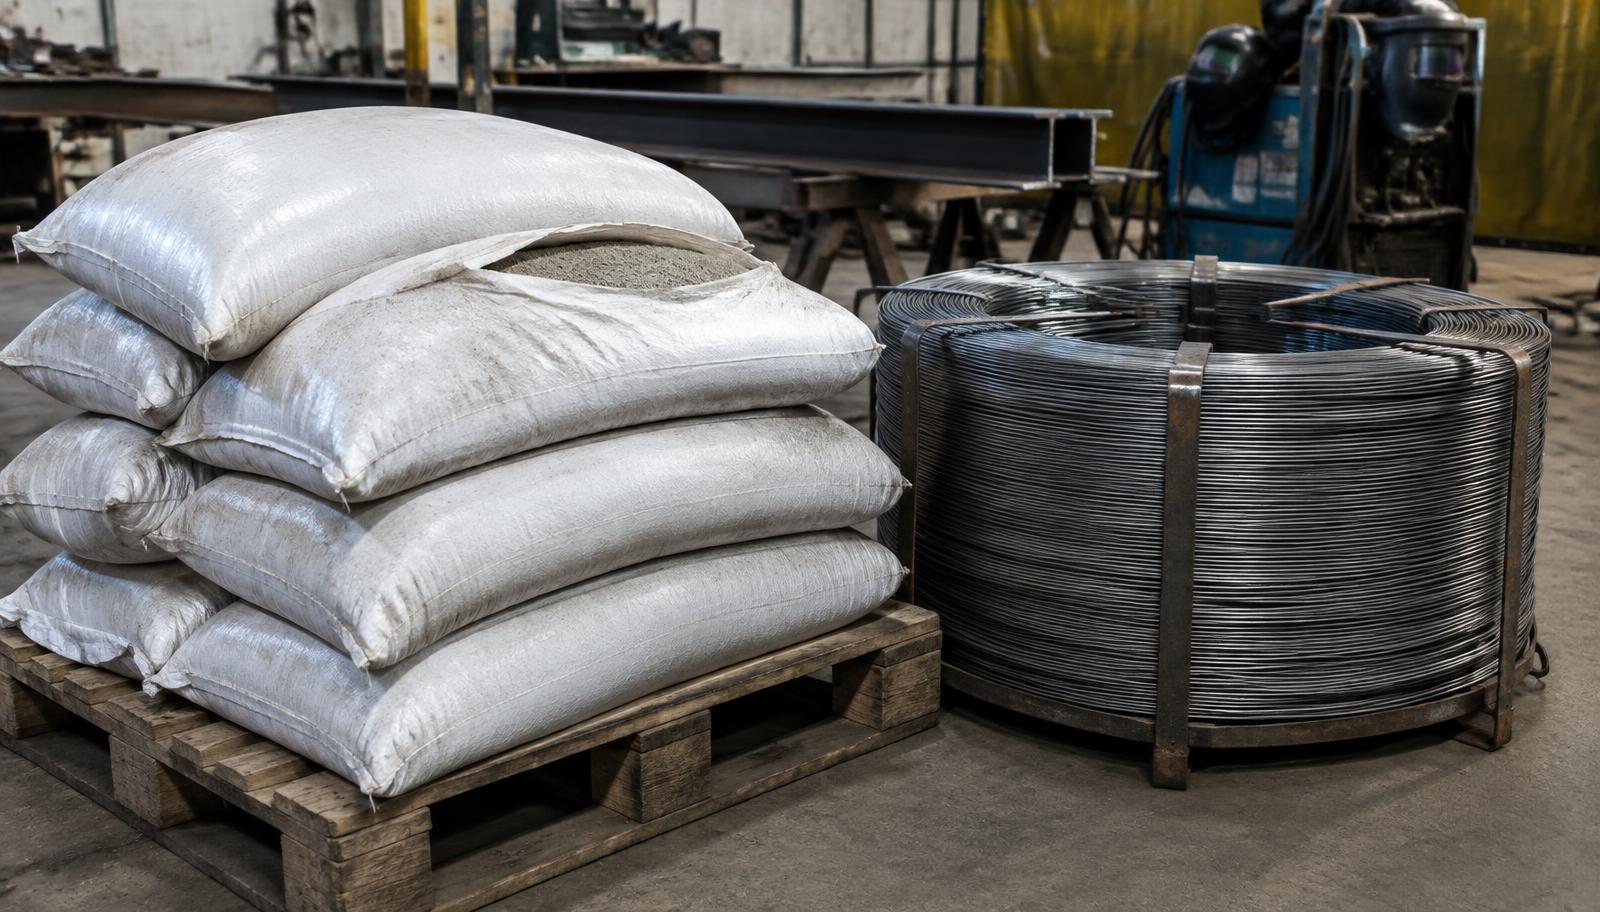
SAW Wire & Flux
Submerged-arc combinations for heavy sections.
Explore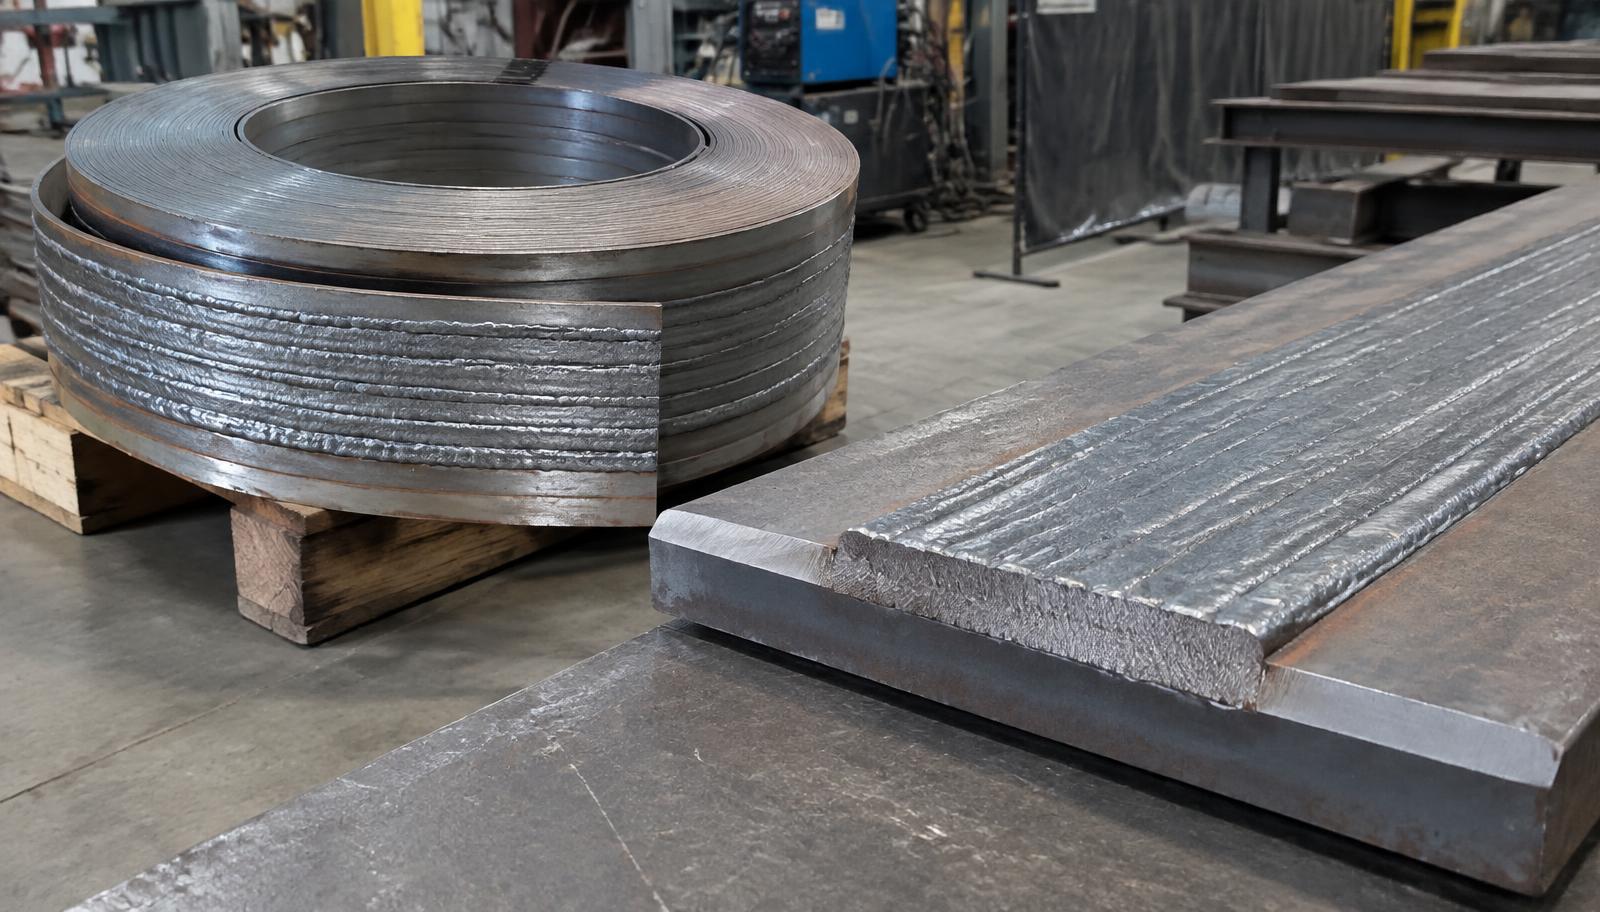
Strip & Overlay
Cladding strip and flux for weld overlay.
Explore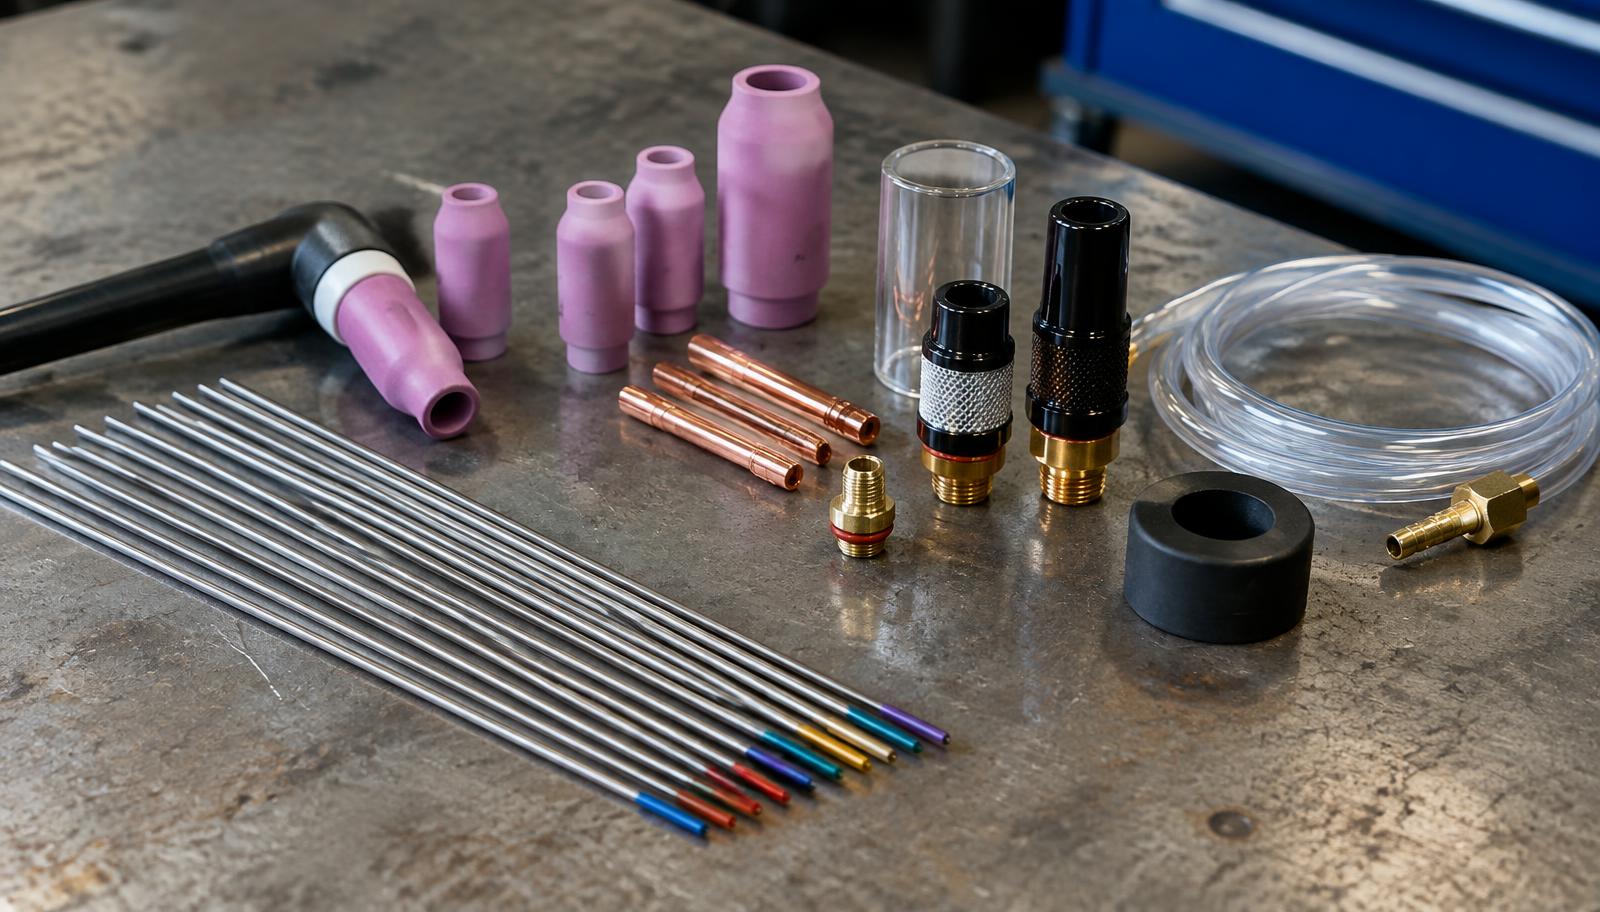
Tungsten Electrodes
Thoriated, ceriated and lanthanated.
Explore
Purge Accessories
Backing tape, purge dams and gas lenses.
ExploreWelding Consumables specifications.
Standards, sizes, thickness and condition we routinely supply across every product form.
| Product | Size Range | Thickness / Wall | Finish / Condition | Standards |
|---|---|---|---|---|
Stainless TIG Wire | Ø 1.6 – 3.2 mm | 1000 mm cut length | Bright drawn, vacuum packed | AWS A5.9 / SFA 5.9 |
Stainless Electrodes | Ø 2.5 – 4.0 mm | 300 / 350 mm length | Rutile / basic coated | AWS A5.4 / SFA 5.4 |
Nickel Alloy Wire | Ø 1.2 – 3.2 mm | Spool or cut length | Bright drawn | AWS A5.14 / A5.11 |
Duplex Wire & Electrodes | Ø 1.2 – 4.0 mm | Spool / cut length | Bright / coated | AWS A5.9 / A5.4 |
Carbon & Alloy Electrodes | Ø 2.5 – 5.0 mm | 350 / 450 mm length | Low-hydrogen basic | AWS A5.1 / A5.5 |
Note: Batch test certificates, ferrite number reports and re-drying instructions supplied with each consignment.
Where welding consumables are used.
Fabrication Shops
General stainless and carbon steel fabrication, tanks and structures.
Oil & Gas
Sour-service welds, CRA overlays and NACE-qualified procedures.
Power & Boilers
P22 and P91 welds with matched B3 and B9 electrodes.
Pharma & Food
Hygienic orbital welds in 316L with purge control.
Shipbuilding & Marine
Duplex, cupro nickel and Monel welds in seawater systems.
Maintenance
Dissimilar-metal repairs with ER309L and nickel-base fillers.
Frequently asked questions.
Answers to the questions our Mumbai desk is asked most often.
Which filler wire should be used for welding 316L?
+
ER316L for TIG and MIG, or E316L-16 covered electrodes for manual welding. The low-carbon filler prevents carbide precipitation in the heat-affected zone. For welding 316L to carbon steel, ER309L is used instead because it tolerates the dilution.
What consumable is used for duplex 2205?
+
ER2209 filler wire and E2209 electrodes. The consumable is deliberately over-alloyed in nickel relative to the parent metal so that the weld metal recovers the correct 50:50 ferrite-austenite balance on cooling. Super duplex 2507 uses ER2594 on the same principle.
Do welding electrodes need re-drying before use?
+
Basic low-hydrogen electrodes such as E7018, E9018-B3 and E9015-B9 must be re-dried at the manufacturer's stated temperature (typically 300–400 °C for one to two hours) and held in a heated quiver. Stainless rutile electrodes require lighter re-drying at around 150 °C. Re-drying instructions ship with every consignment.
Every dispatch is traceable, tested and certified.
Material is supplied with EN 10204 3.1 (3.2 on request) mill test certificates, PMI and spectro verification, and is open to third-party inspection by TUV, SGS, BV, Lloyd’s and IRS from our Mumbai warehouse.
EN 10204 3.1 / 3.2
Mill test certificate with every consignment.
PMI & Spectro
Positive material identification before dispatch.
Third-party Inspection
TUV · SGS · BV · Lloyd's · IRS welcome.
Export Documentation
Full set prepared for 40+ countries.
Other grades you may also need
Ready to price your requirement?
Share your grade, form, size and quantity — our Mumbai desk responds with pricing, stock position and lead time, usually the same working day.